01 Hygiene and Quality Stability
Improving Consistency in Cooking and Packaging Quality
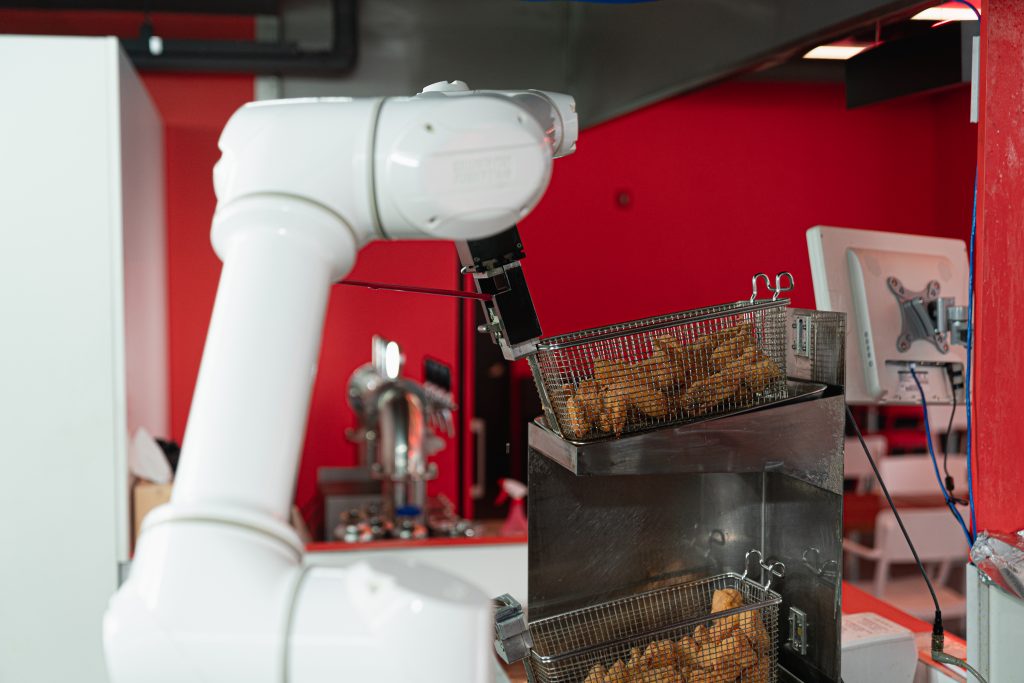
Across food manufacturing, cooking, packaging, and in-store serving, robot automation helps secure hygiene, safety, speed, and consistency.
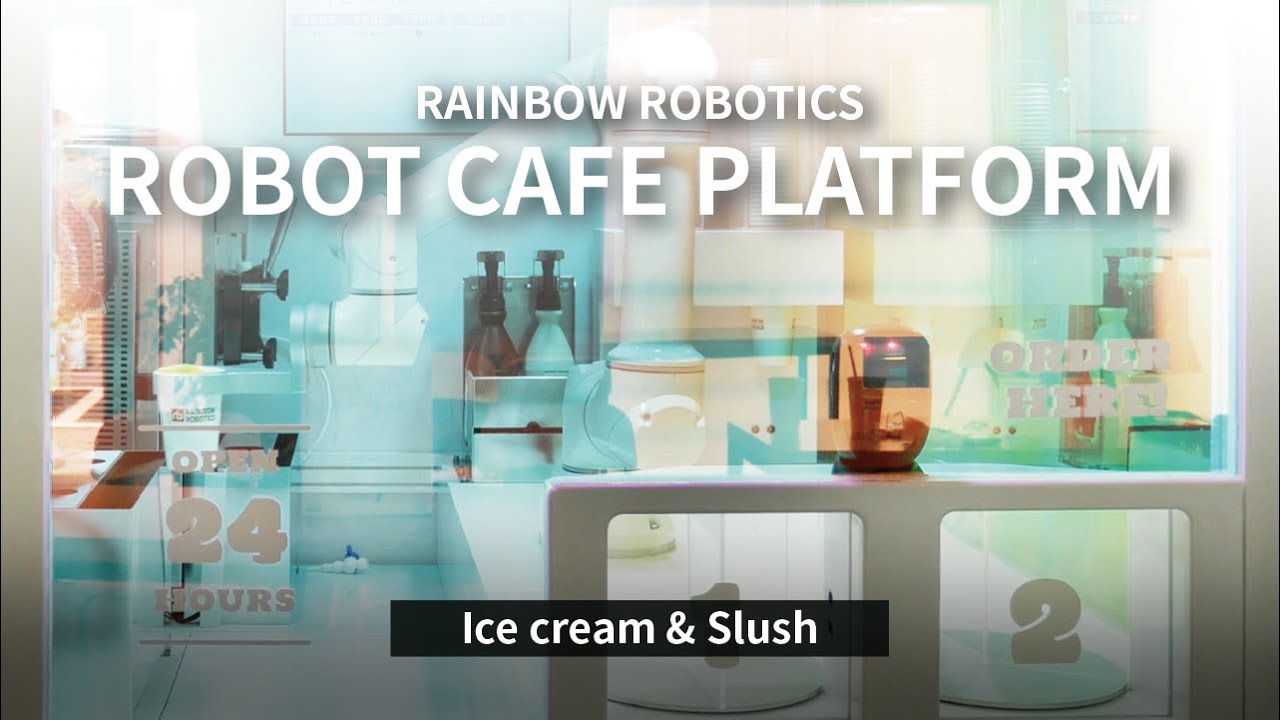
Rainbow Robotics supports diverse F&B automation using collaborative robots, AMRs, and mobile dual-arm robots.
Key Benefits
Improving Consistency in Cooking and Packaging Quality
Increased productivity through automation of repetitive and high-speed tasks &
Working simultaneously with people even in cramped stores and kitchens
Minimizing hazardous operations such as high temperatures, oil exposure, and heavy lifting
Improving customer experience through faster and more accurate serving
Technology Highlights
Rainbow Robotics supports F&B applications from collaborative-robot cooking and packaging to AMR serving and precise dual-arm handling.
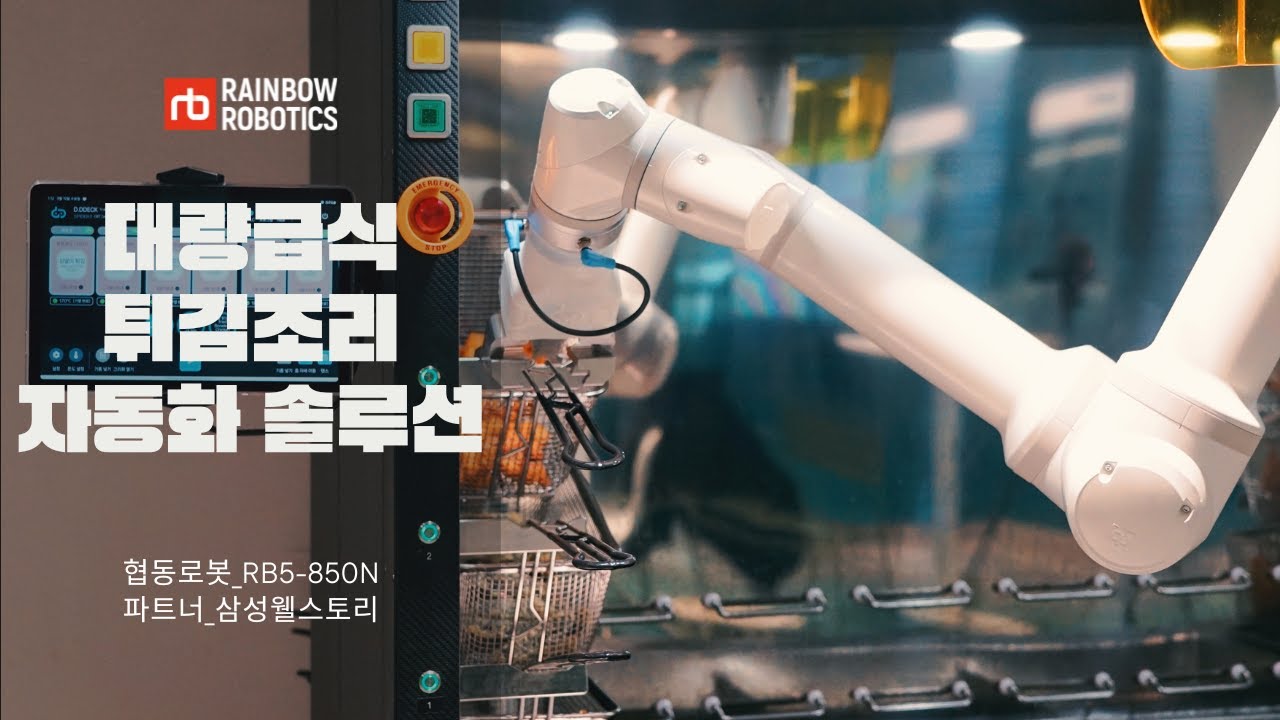
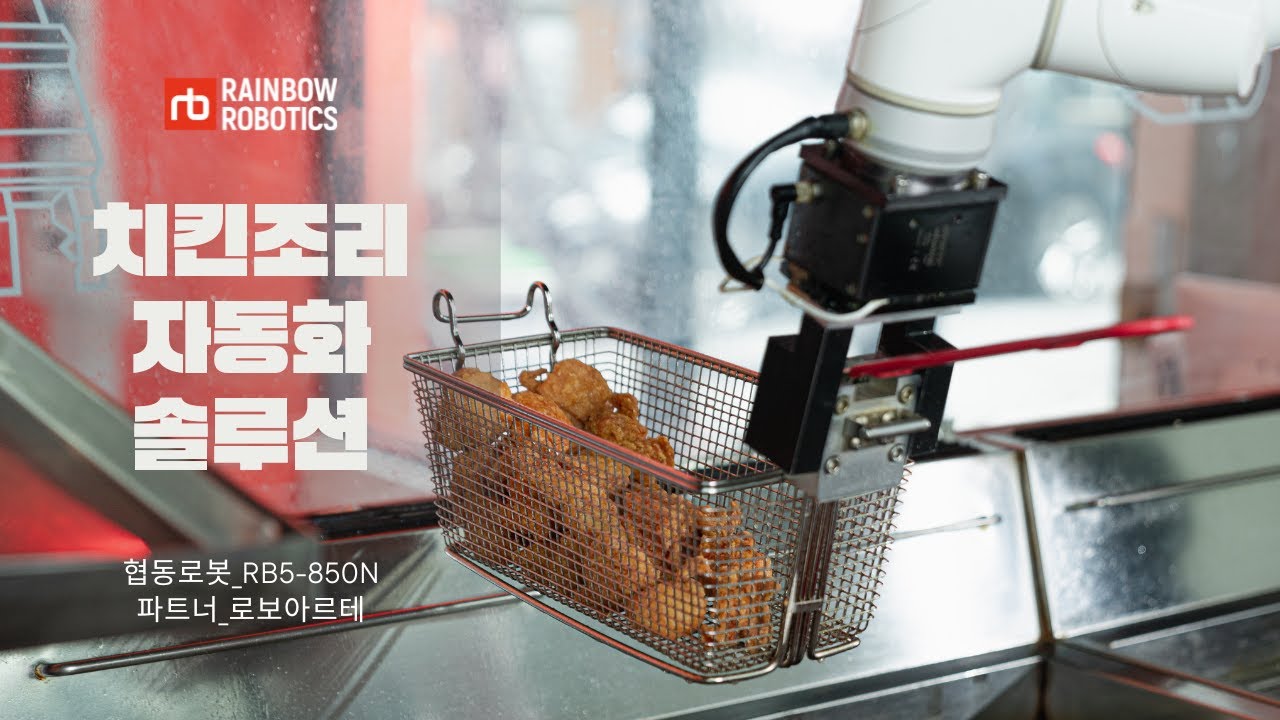
By utilizing robots, even high-temperature cooking tasks such as frying, grilling, and stir-frying can be carried out with precise control of timing, path, and force
You can maintain the recipe standards consistently. Mobile dual-arm robots and collaborative robots reliably replicate the repetitive movements of the human hand, significantly reducing variations in taste, texture, and cooking quality.

Food preparation environments are characterized by many unfavorable factors for robot actuators, such as high temperature, high humidity, vapor, and oil splashes.
Rainbow Robotics’ RB-N series collaborative robots offer the highest IP66-rated dust and water resistance among comparable models, making them suitable even for kitchen and food manufacturing environments where high-pressure steam, frying oil, and washing water are repeatedly exposed
It can operate stably.

Even in tasks requiring sorting, classification, and stacking, such as lunchbox production, product packing, and container filling
Ensures stable packaging quality through vision-based position correction and precise gripper control.
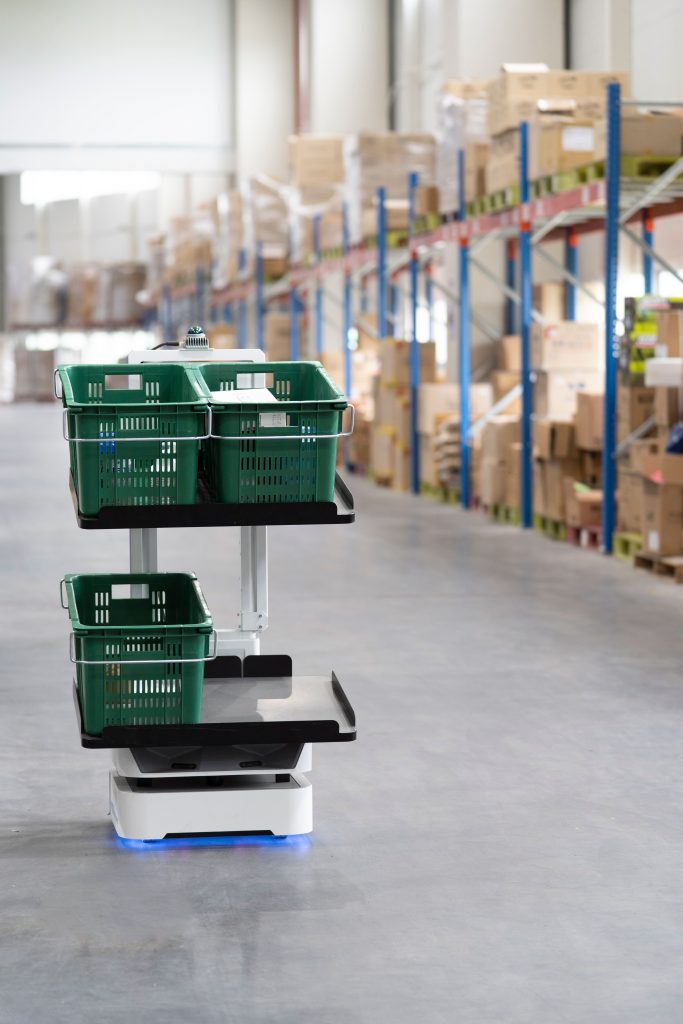
It is also possible to create a flow that links cooking, packaging, and shipping in conjunction with AMR.

AMR moves safely even in crowded environments, thanks to its in-store location-based map and obstacle detection capabilities.
Automate repetitive tasks such as serving, dish collection, and moving between tables to reduce employees’ workload and help them focus on customer service.

Rainbow Robotics’ robots can be installed in various locations such as restaurant floors, ceilings, and walls, and are designed to be used as a single product without needing to be covered with a robotic jacket or additional accessories, making it easy to integrate with existing systems where F&B services are required.